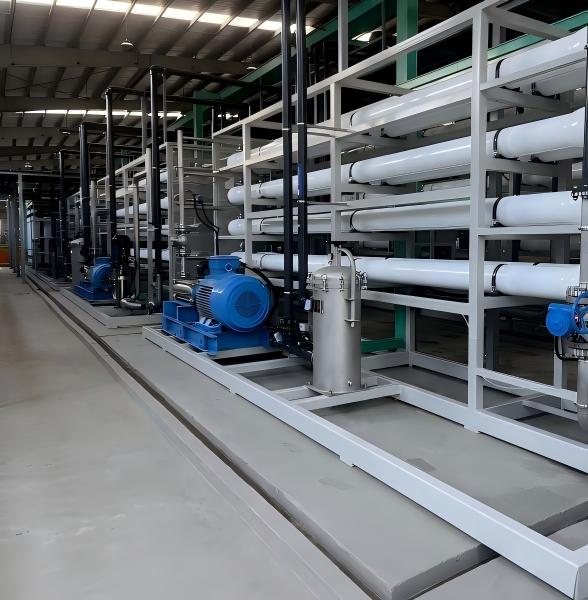
PLC Control in Block Making Machines How Automation Improves Consistency

Quick Answer

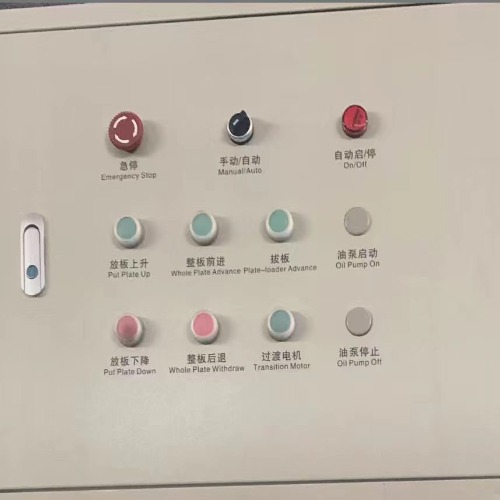
PLC (Programmable Logic Controller) control systems are revolutionizing block making by replacing manual operations with precise, automated sequences that dramatically improve product consistency. Research shows that PLC-based automation can reduce cycle time by 15.4% and increase production by 300 pieces per hour compared to manually operated machines. By standardizing mix ratios, vibration parameters, and pressing pressure, PLC systems eliminate human error, ensuring uniform density, dimensional accuracy, and compressive strength across every batch . Modern PLC systems with touchscreen interfaces also enable real-time monitoring, fault diagnosis, and recipe storage for different block types, making them essential for block plants seeking quality consistency and operational efficiency.
 

  •  
  •  
  •  

--------------占位---------------


1. User Search Intent Analysis

Who Is Searching and Why?

Audience Primary Intent Key Concerns
Production Managers Operational/Decision How automation reduces defects and improves output consistency
Engineers Technical/Informational PLC programming, system integration, control logic
Plant Owners Commercial/ROI Cost-benefit analysis, payback period, labor savings
Quality Control Staff Informational/Procedural How PLCs ensure batch-to-batch uniformity


Search Intent Categories Informational: Understanding PLC functions, automation benefits, and implementation Commercial: Evaluating automation investment, comparing PLC vs. manual systems Technical: Learning about control logic, sensors, and system integration Problem-solving: Addressing quality inconsistency, human error, and productivity issues.


2. Key User Questions

Quality & Consistency Questions

"How does PLC control improve block quality?" — Standardizes mix ratios, pressure, and vibration to reduce human error "Can PLC systems reduce defect rates?" — Yes, PLC-based interlock systems have shown to reduce product failure rates by 13% "How does automation affect block density and strength?" — Uniform compaction produces higher compressive strength and better surface finish.

Technical Questions

"What does a PLC system in a block machine consist of?" — PLC controller, sensors, hydraulic actuators, HMI touchscreen, and programming software "How are PLCs programmed for block machines?" — Using ladder logic, structured text, or function blocks conforming to IEC 61131-3 standards "Can PLCs handle different block types?" — Yes, recipe storage allows one-touch switching between hollow blocks, solid bricks, pavers, and curbstones.

Operational Questions

"How much can PLC automation increase production?" — Studies show cycle time reduction of 15.4% and production increase of 300 pcs/hour "What maintenance is required for PLC systems?" — Regular checks on electrical connections, sensor calibration, and software updates "Is operator training difficult?" — Modern systems feature user-friendly HMI interfaces requiring minimal technical expertise.


3. How PLC Control Works in Block Making

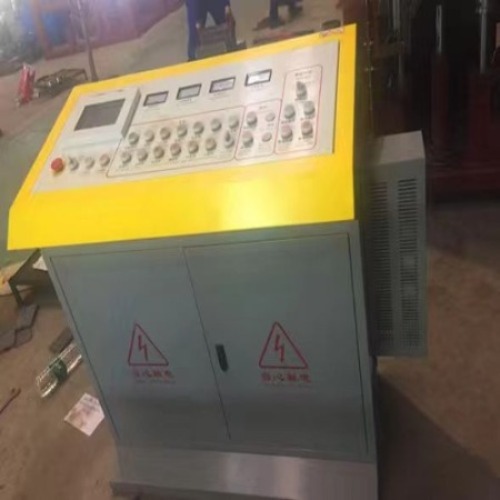
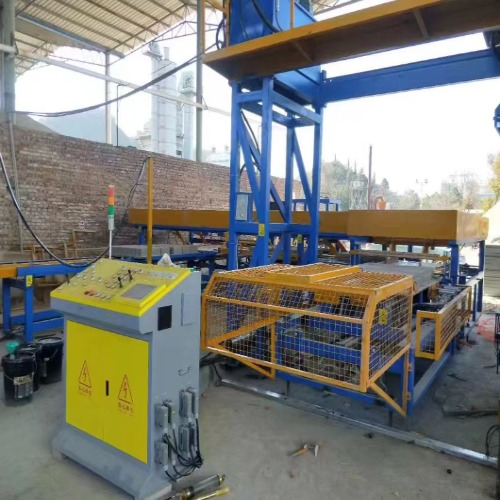
The Automation Architecture A PLC-based control system in a block making machine integrates multiple subsystems through a central processing unit : The PLC Controller serves as the system's brain, executing programmed logic that coordinates all production steps. Conforming to IEC 61131-3 standards, modern PLCs allow engineers to create reusable function blocks that increase programming efficiency and reliability . Sensors and Inputs monitor critical parameters: material levels, hydraulic pressure, temperature, vibration frequency, and mold position. Real-time feedback enables dynamic adjustments during each production cycle . Actuators and Outputs translate control signals into mechanical actions: hydraulic press movement, vibration activation, material feeding, and block ejection. High-precision components like proportional valves ensure accurate control . Human-Machine Interface provides operators with a touchscreen panel for monitoring, parameter adjustment, recipe selection, and fault diagnosis. This reduces reliance on operator experience and ensures repeatability . The Production Cycle Under PLC Control From raw material to finished block, the PLC manages each step with precision : Batching: PLC controls weighing systems to ensure accurate material proportions Mixing: Timing and mixing intensity regulated for consistent concrete Molding: PLC coordinates vibration frequency, amplitude, and pressing pressure Ejection: Demolding sequences synchronized for damage-free removal Stacking: Automatic palletizing and stacking controlled by the PLC.


4. How PLC Control Improves Consistency

Elimination of Human Error Manual machines rely on operator judgment for mix ratios, vibration duration, and pressure application—variables that naturally fluctuate. PLC systems eliminate this variability by executing the same precise sequence every cycle . Research confirms that conventional paving block machines are "prone to human error and being less consistent" . PLC automation directly addresses this by standardizing the entire production process . Standardized Parameters PLC control ensures that every block experiences identical: Mix proportions: ±1% accuracy in material dosing Vibration intensity: Uniform frequency and amplitude per cycle Pressing force: Consistent hydraulic pressure application Cycle timing: Repeatable filling, compaction, and ejection sequences This standardization results in uniform density, dimensional accuracy, and compressive strength across all production . Real-Time Quality Monitoring Modern smart control systems incorporate feedback loops that adjust parameters dynamically based on real-time data . When deviations in cycle time or energy consumption occur, the system can detect and correct them instantly, often before operators are aware of the issue . This predictive capability enables: Immediate detection of quality deviations Automatic parameter correction Prevention of defective batches Reduced material waste.


5. Measurable Benefits of PLC Automation

Productivity Gains Research on PLC-modified paving block machines shows concrete results: cycle time decreased by 15.4%, leading to production increases of 300 pieces per hour compared to manual operation . Quality Improvement PLC-based control systems have demonstrated defect reduction of 13% through precise interlock programming . Fully automatic PLC-controlled machines maintain defect rates below 1%, compared to 2-3% for manual operations . Operational Efficiency Labor reduction: Fully automatic systems require only 3-5 workers vs. 8-12 for manual lines Energy savings: Optimized cycles reduce power consumption Waste reduction: Precise batching minimizes material waste Consistency: Uniform quality across all production batches.


6. Implementation Considerations

Initial Investment PLC-controlled block machines require higher upfront investment compared to conventional systems. However, the ROI is achieved through reduced labor costs, lower defect rates, and higher production capacity . Studies indicate that fully automatic lines often recover investment in 6-10 months. Training Requirements Modern PLC systems feature user-friendly HMI interfaces, allowing operators to manage complex processes with minimal technical expertise . However, maintenance staff require technical training for PLC programming and troubleshooting . Mold Compatibility Even the most advanced PLC system requires high-quality molds to achieve consistency . Molds should be heat-treated for wear resistance and designed for accurate fitting, smooth demolding, and consistent block geometry .


7. Future Trends: Smart Control in Block Manufacturing

The evolution of PLC control is moving toward fully integrated smart manufacturing systems : Predictive Maintenance: Systems that identify inefficiencies and implement corrective measures proactively Remote Monitoring: Cloud-based access to production data IIoT Integration: Connecting machines to enterprise systems for real-time optimization Self-Optimization: Systems that adjust parameters autonomously based on material behavior As one industry expert notes, smart control "transforms machines into responsive systems, production lines into intelligent networks, and manufacturing itself into a continuously evolving discipline" .


8. FAQ


1. What is a PLC in a block making machine?

A Programmable Logic Controller (PLC) is an industrial computer that automates the block production process. It controls batching, mixing, molding, and stacking through programmed logic, replacing manual operation and relay-based control .

2. How does PLC control improve block quality?

PLC systems standardize mix ratios, vibration parameters, and pressing pressure, eliminating human error. Research shows PLC automation can reduce defect rates by up to 13% and ensure uniform density and strength across all batches .

3. What production improvements can I expect with PLC automation?

Studies demonstrate 15.4% cycle time reduction and production increases of 300 pieces per hour compared to manual operation . Fully automatic PLC lines can achieve 10,000+ blocks per shift with only 3-5 workers.

4. Is PLC control suitable for small block plants?

Yes. Scalable PLC systems can be implemented in various production environments, offering efficiency gains regardless of plant size . Semi-automatic configurations with basic PLC control are available for lower-volume operations.

5. How difficult is it to operate a PLC-controlled block machine?

Modern systems feature user-friendly touchscreen interfaces that allow operators to monitor and adjust production with minimal technical expertise . However, maintenance staff require technical training for system diagnostics and programming .

6. Can a PLC system handle different block types?

Yes. PLCs store recipes for different block types—hollow blocks, solid bricks, pavers, and curbstones—allowing one-touch switching between products .

7. What maintenance is required for PLC control systems?

Regular checks on electrical connections, sensor calibration, and software updates are essential. Worn components should be replaced according to inspection results and working hours .


If you want to get more information about our products, you can click www.yxbrickequipment.com
 

Short Lifespan of Brick Machine Molds? 3 Tips to Choose the Right Wear-Resistant Materials

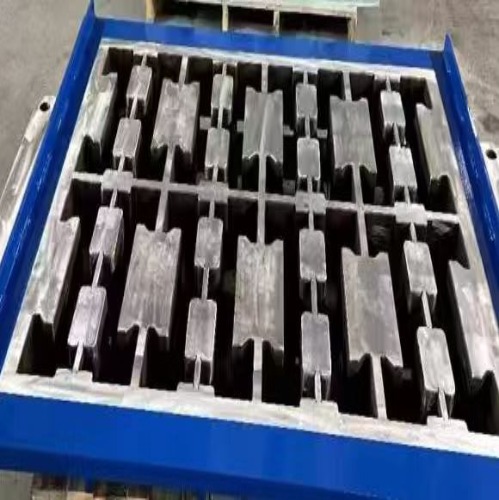
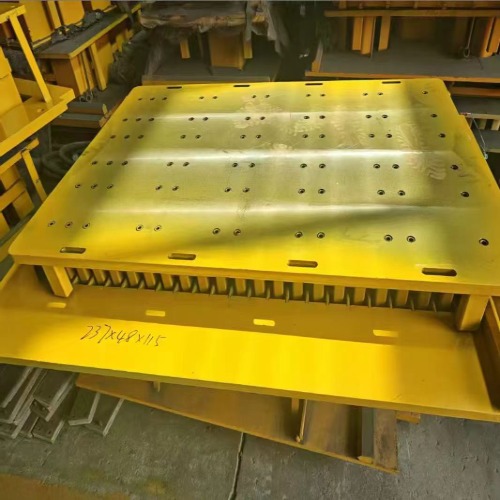
In the production of concrete blocks and refractory bricks, molds are one of the most vulnerable parts and represent the largest operating cost of production equipment. The root cause of brick machine mold wear lies in abrasive wear—hard particles in the brick material (such as quartz, feldspar, etc.) rub intensely against the mold surface during the molding process, causing the surface material to gradually peel off. When the mold surface wear reaches 0.3-0.4mm, the brick blank dimensions will be out of tolerance, resulting in quality problems such as cracks, chipped edges, and corner damage, necessitating replacement or repair. So, how can we solve the problem of short mold lifespan from the material perspective? The following three tips will help you choose the right wear-resistant materials.


Tips 1: Understand the "Levels" of Mainstream Mold Materials

The most crucial requirement for brick machine mold materials is wear resistance, while strength, toughness, and process feasibility must also be considered. Currently, mainstream mold materials can be divided into three levels:

Entry-level:Carbon steel and alloy steel: Represented by low and medium carbon steel, surface hardness is improved through gas carbonitriding heat treatment (reaching HRC 60-64). They are inexpensive and widely used, but their lifespan is relatively limited. These materials are suitable for small- to medium-scale production with small batch sizes.

Advanced-level:High-chromium alloys and mold steels: Such as high-chromium alloy steel and high-chromium cast iron, their wear resistance is significantly better than ordinary carbon steel. Comparative studies have found that H13 steel exhibits excellent wear resistance among hot-work mold steels. These materials are suitable for medium to large-sized brick factories with specific requirements for mold lifespan.

High-end:Hard alloys and steel-bonded hard alloys: This is currently recognized as the best wear-resistant solution. GT35 steel-bonded hard alloy is particularly noteworthy—it uses steel as the binder phase and titanium carbide as the hard phase, combining the machinability of tool steel with the high hardness of hard alloys (HRC can reach 68-72 after heat treatment), with a density of only 6.4 g/cm³, and can be used to manufacture complex, irregularly shaped molds.


The Second Strategy: Carbide Inlay – The Secret to 60-100 Times Longer Lifespan

If choosing high-grade materials is an "upgrade," then carbide inlay technology is a "qualitative leap."

Inlay Process: A 10-200mm thick tungsten carbide alloy block (such as YG15) or steel-bonded carbide block (such as GT35) is inlaid into the worn areas of the mold. After adhesive bonding and precision grinding, it is installed into the mold frame for use.

Lifespan Comparison: Research data from Science Popularization China shows that the lifespan of carbide-inlaid molds is 60-100 times longer than that of ordinary carbon steel molds. Furthermore, after each wear event, the marks can be ground away and the mold can be reassembled for reuse, with a single mold piece being reusable approximately 10 times.

Although carbide materials are expensive, the unit production cost is actually lower – making it especially suitable for high-volume, long-term continuous production scenarios.


The Third Strategy: The "Nice Finishing Touch" of Process and Design

Besides choosing the right material, process and design can also significantly extend mold lifespan:

Surface Strengthening Treatment: Surface treatments such as carbonitriding and chromium infiltration on ordinary steel molds can significantly improve surface hardness. Studies have reported that the service life of chromium-infiltrated cast iron brick-making molds is 8-10 times that of modified cast iron molds.

Mold structure optimization: For example, moving the brick forming position of the brick press upwards allows the mold to be reused after wear, with each side usable twice, effectively extending its lifespan. This approach also applies to the layout design of the mold's inlaid alloy blocks—placing the alloy blocks in the areas of highest wear to maximize material utilization.

Reusing used molds: Severely worn but not yet scrapped molds can be re-ground or have their inlaid blocks replaced for continued use, reducing the cost of purchasing new molds.

  •  
  •  
  •  


 Extending the lifespan of brick machine molds hinges on selecting the right materials, using the right processes, and designing correctly. For brick factories with large-scale, continuous production, directly choosing hard alloy inlaid molds, although requiring a higher initial investment, is the optimal solution for cost reduction in the long run. For small- to medium-scale production, high-chromium alloys combined with surface strengthening treatment are a pragmatic choice that balances cost-effectiveness. Choosing the right mold material is crucial to truly addressing your "lifespan shortcoming."

How Industrial Water Recycling Supports Sustainable Manufacturing

Manufacturing industries are facing increasing challenges in water management. Rising water demand, stricter environmental regulations, and the need for sustainable production are driving companies to rethink how they use and manage water resources.


Industrial water recycling provides an effective solution by treating wastewater generated during production processes and converting it into reusable water. Instead of discharging wastewater after a single use, manufacturers can recover valuable water resources and create a more sustainable production cycle.


Why Industrial Water Recycling Matters for Modern Manufacturing

Many industries, including new energy, semiconductor, electronics, electroplating, and chemical manufacturing, consume large amounts of water during production. At the same time, their wastewater may contain high levels of dissolved salts, heavy metals, or other complex contaminants.


A well-designed industrial wastewater treatment system can help companies:

  • Reduce freshwater consumption
  • Lower wastewater discharge volume
  • Improve environmental compliance
  • Recover reusable process water
  • Support long-term sustainable manufacturing goals


Advanced treatment technologies such as ultrafiltration (UF), reverse osmosis (RO), nanofiltration (NF), and zero liquid discharge (ZLD) are commonly integrated according to wastewater characteristics and reuse requirements.


Industrial Water Recycling Solution for New Energy Industry

As a wastewater treatment solution provider, Eragon Enviro Tech has developed water recycling systems for industries with challenging wastewater conditions.


For example, in a new energy industry wastewater reuse project, the wastewater contained high salinity and required stable treatment performance. The system adopted membrane-based treatment technologies, including pretreatment, UF and RO processes, to recover reusable water and support a zero liquid discharge (ZLD) target.


Through optimized process design, the treated water can be reused in production, reducing dependence on fresh water sources and improving overall resource efficiency.

Industrial wastewater reuse solution for sustainable manufacturing

(Internal link: Industrial Wastewater Reuse & ZLD Project)


Building a More Sustainable Water Future

Industrial water recycling is not only an environmental solution but also a strategy for improving operational efficiency.


For manufacturers, the right wastewater treatment technology can transform wastewater from a disposal challenge into a valuable resource. By combining water reuse systems, wastewater recycling technologies, and ZLD solutions, companies can move closer to a circular water management model.


With more than 20 years of industry experience, Eragon Enviro Tech provides customized wastewater treatment solutions for global customers, helping industries achieve reliable water reuse and sustainable development.

Industrial water recycling system for new energy wastewater treatment

(Internal link: Industrial Water Recycling Solutions)


FAQ

What is industrial water recycling?

Industrial water recycling is the process of treating wastewater generated from manufacturing processes and reusing the recovered water for production or other industrial applications.


Which industries need industrial water recycling systems?

Industries such as semiconductor manufacturing, battery production, electroplating, electronics, chemical processing, and metal finishing often require advanced water recycling solutions.


What technologies are used in industrial water recycling?

Common technologies include UF, RO, NF, MBR, evaporation, and ZLD systems. The selection depends on wastewater quality and water reuse requirements.

How Membrane Technology Is Transforming Industrial Water Reuse

Industrial water reuse is no longer just an environmental initiative—it has become a practical strategy for manufacturers facing rising water costs, stricter discharge regulations, and sustainability targets. Over the past two decades, membrane technology in wastewater treatment has fundamentally changed how industries manage and recycle water.


Today, technologies such as ultrafiltration (UF), nanofiltration (NF), and reverse osmosis (RO) enable facilities to recover high-quality water from complex industrial wastewater streams that were previously considered difficult to treat.


In practical engineering applications, selecting the best membrane system for wastewater recycling depends not only on water quality but also on long-term operational stability. Systems designed purely for high recovery without considering fouling risks often face performance decline within the first year of operation.


Why Membrane Technology Is Central to Water Reuse

Traditional wastewater treatment processes often rely on sedimentation, biological treatment, and chemical precipitation. While these processes remove many pollutants, they usually cannot produce water clean enough for reuse in industrial processes.


Membrane filtration works differently. It uses semi-permeable membranes to physically separate contaminants based on size and charge, allowing water molecules to pass while rejecting dissolved salts, heavy metals, and organic compounds.


Because of this capability, industrial membrane filtration systems are now widely used in sectors such as:

  • Electroplating and surface treatment
  • Semiconductor manufacturing
  • Chemical processing
  • Textile and dye production


These industries often generate wastewater with high salinity, heavy metals, or complex contaminants, making membrane-based treatment essential for reliable water recycling.


⇒Learn more about membrane technologies:

Industrial RO Membranes


From Wastewater to Reusable Process Water

One of the most significant advantages of membrane technology is its ability to transform wastewater into high-quality reusable water.


In a plating industrial park wastewater reuse project, wastewater contained fluctuating concentrations of heavy metals and dissolved salts from surface finishing processes. The treatment system combined chemical pretreatment with ultrafiltration and reverse osmosis membranes.


During initial operation, engineers observed rapid pressure increases in the RO units. Investigation showed that the root cause was unstable pretreatment rather than membrane failure. After optimizing solids removal and chemical dosing control upstream, the membrane system stabilized and achieved the target water recovery rate for industrial reuse.


This project highlighted a key engineering principle: membrane performance depends heavily on effective pretreatment design.


Today, the recovered water is reused within the facility for production processes, significantly reducing freshwater consumption and wastewater discharge.


Improving Water Recovery Rates

Compared with traditional treatment processes, membrane filtration offers a more predictable and controllable solution for industries seeking high recovery water reuse system design, especially in applications with strict reuse standards.


Reverse osmosis systems, for example, can remove over 95% of dissolved salts and contaminants, producing permeate suitable for many industrial applications.


In many reuse systems, membrane processes are combined with thermal technologies to achieve even higher recovery rates. For facilities aiming to approach zero liquid discharge (ZLD), membrane separation is often the first stage that concentrates contaminants before evaporation or crystallization.


This layered treatment approach allows plants to maximize water reuse while controlling operating costs.


Supporting Sustainable Manufacturing

Beyond technical performance, membrane-based water reuse systems support broader sustainability goals in industrial operations.


By recycling treated wastewater, manufacturers can:

  • Reduce freshwater intake
  • Lower wastewater discharge volumes
  • Improve compliance with environmental regulations
  • Stabilize long-term operating costs


For industries operating in water-scarce regions or under strict discharge limits, industrial water recycling systems based on membrane technology are increasingly becoming a strategic investment rather than an optional upgrade.


Engineering Perspective

From an engineering standpoint, membrane technology is most effective when integrated into a well-designed treatment train.


A typical industrial water reuse system may include:


Coagulation → Clarification → Filtration → Membrane Separation (UF/RO) → Reuse


When each stage is properly designed and controlled, membrane systems can operate reliably for years while delivering consistent water quality.


For companies planning new water reuse projects, the key is not simply choosing a membrane product but designing a system that considers pretreatment, scaling control, and long-term operation.


FAQ

Q: How does membrane technology improve industrial water reuse?

A: Membrane technology removes dissolved salts, heavy metals, and fine particles that conventional treatment cannot eliminate, allowing treated water to be reused in industrial processes.


Q: What is the best membrane system for wastewater recycling?

A: The best system depends on wastewater characteristics, but most industrial applications use a combination of ultrafiltration (UF) and reverse osmosis (RO) for optimal performance.


Q: Can membrane systems achieve zero liquid discharge?

A: Membrane systems are typically used as a pretreatment step in ZLD systems, concentrating wastewater before evaporation or crystallization.

How to Reduce Operating Costs in Industrial Water Treatment Systems

Operating costs are one of the most critical concerns in industrial water treatment projects. While initial system design often focuses on meeting discharge or reuse standards, long-term performance is ultimately defined by operating cost efficiency.


In practice, reducing industrial water treatment operating costs is not about cutting corners—it is about optimizing system design, improving stability, and selecting the right technologies based on actual wastewater characteristics.


Optimize Pretreatment to Avoid Downstream Costs

One of the most overlooked factors affecting wastewater treatment operating cost reduction is pretreatment design.


In a surface treatment industrial wastewater project, early operation showed frequent membrane fouling and unstable performance. Investigation revealed that incomplete removal of suspended solids and oil residues was causing excessive load on the downstream system.


After optimizing coagulation, flocculation, and solid–liquid separation, the system became significantly more stable. As a result:

  • Chemical consumption decreased
  • Membrane cleaning frequency was reduced
  • System downtime was minimized


This highlights a key engineering principle: a well-designed pretreatment stage can significantly reduce long-term operating costs.


Improve Water Recovery Efficiency

Improving water recovery rates in industrial wastewater treatment is another effective way to reduce costs.


Higher recovery means:

  • Lower freshwater consumption
  • Reduced wastewater discharge volume
  • Lower disposal costs


Technologies such as reverse osmosis (RO) are widely used to maximize water recovery. However, pushing recovery too high without proper design may lead to scaling and higher maintenance costs.


⇒Learn more about:

Industrial Reverse Osmosis Systems


From an engineering perspective, the goal is to find the optimal recovery balance, not simply the highest possible recovery.


Control Energy Consumption in Advanced Treatment

Energy consumption is a major contributor to industrial wastewater treatment operating expenses, especially in systems involving evaporation.


For high-salinity wastewater or ZLD systems, MVR (Mechanical Vapor Recompression) evaporation technology is often used because it is significantly more energy-efficient than traditional thermal evaporation.


⇒Related technology:

MVR Evaporation Systems


In one project, integrating membrane concentration before evaporation reduced the volume of wastewater entering the evaporator. This design change significantly lowered energy consumption and improved overall system efficiency.


This reflects a common optimization strategy: reduce load on high-energy processes by improving upstream efficiency.


Design for Stable Operation, Not Just Capacity

Many systems are designed based on peak capacity, but real operating conditions often fluctuate. Systems that perform well on paper may face instability in actual operation.


Unstable systems typically lead to:

  • Increased chemical dosing
  • Higher energy use
  • Frequent maintenance


In our project experience, systems designed with buffer capacity, proper equalization, and flexible control strategies consistently show lower operating costs over time.


Stability is one of the most important—and often underestimated—factors in cost control.


Select the Right Technology for the Application

There is no single "best" technology for all wastewater treatment systems. Choosing the wrong process can significantly increase operating costs.


For example:

  • Using advanced treatment where simple clarification is sufficient increases unnecessary cost
  • Relying only on membranes for high-salinity wastewater may lead to frequent scaling issues
  • Ignoring concentrate management can create hidden long-term costs


The key is to match the technology to the actual wastewater characteristics and treatment objectives.


Engineering Perspective

In practice, reducing industrial water treatment system costs is a result of multiple small optimizations rather than one major change.


Systems that achieve low operating costs typically share these characteristics:

  • Efficient and stable pretreatment
  • Balanced water recovery design
  • Optimized energy use in advanced processes
  • Integration between process stages
  • Long-term operational stability


Facilities that focus only on initial capital cost often face higher expenses later, while those that prioritize system design and operation tend to achieve better overall performance.


FAQ

Q: What is the biggest factor affecting wastewater treatment operating costs?

A: Pretreatment efficiency and system stability are often the biggest factors, as they directly impact chemical use, energy consumption, and maintenance frequency.


Q: How can energy costs be reduced in wastewater treatment systems?

A: Energy costs can be reduced by optimizing process design, improving upstream efficiency, and using energy-efficient technologies such as MVR evaporation.

RO vs Evaporation Which Technology Is Better for High-Salinity Wastewater?

High-salinity wastewater is one of the most difficult challenges in industrial water treatment. As industries push for higher water recovery and stricter discharge compliance, selecting the right technology becomes critical. The debate between RO vs evaporation for high-salinity wastewater treatment is common—but in practice, the answer is rarely one or the other.


Understanding the strengths and limitations of each approach is essential for designing an efficient and reliable system.


What RO Can and Cannot Do

Reverse osmosis (RO) is widely used in industrial wastewater treatment systems due to its ability to remove dissolved salts and produce high-quality permeate.


For moderate salinity wastewater, RO offers:

  • High water recovery
  • Lower energy consumption compared to thermal processes
  • Compact system footprint


⇒Learn more about:

Industrial Reverse Osmosis Systems


However, RO has limitations when dealing with high TDS wastewater. As salinity increases, osmotic pressure rises, reducing recovery rates and increasing the risk of scaling and fouling.


In practical terms, RO is effective up to a certain threshold. Beyond that, performance becomes unstable and operating costs increase.


When Evaporation Becomes Necessary

Evaporation technologies, particularly mechanical vapor recompression (MVR) systems, are designed to handle wastewater that membranes cannot treat efficiently.


For high-salinity or brine streams, evaporation provides:

  • Near-complete separation of water and dissolved solids
  • High recovery rates (approaching ZLD)
  • Ability to handle complex and variable wastewater


The trade-off is energy consumption. Evaporation is typically more energy-intensive than RO, which makes it less suitable as a standalone solution when salinity is still manageable by membranes.


Practical Insight: Why Hybrid Systems Work Best

In one industrial wastewater project involving surface treatment processes, wastewater contained heavy metals and high levels of dissolved salts. The initial design relied heavily on membrane treatment for water recovery.


While RO performed well at the beginning, increasing salinity in the system led to reduced recovery and frequent cleaning requirements.


After integrating an evaporation stage for concentrate treatment, the system achieved stable performance and higher overall recovery.


This reflects a common engineering conclusion:

RO and evaporation are not competing technologies—they are complementary.


Choosing the Right Approach

When evaluating RO vs evaporation for industrial wastewater treatment, the decision depends on several factors:


1. Salinity Level

  • Moderate salinity → RO is more efficient
  • High salinity → Evaporation becomes necessary


2. Water Recovery Targets

  • Standard reuse → RO may be sufficient
  • High recovery or ZLD → Evaporation is required


3. Operating Cost Considerations

  • RO → Lower energy, higher sensitivity to fouling
  • Evaporation → Higher energy, more stable at high salinity


4. Wastewater Complexity

  • Stable composition → RO performs well
  • Variable or complex streams → Hybrid systems are more reliable


Based on our previous projects, the most effective solution for high-salinity wastewater treatment is often a hybrid system:

Pretreatment → Filtration → RO → Evaporation


RO reduces the volume of water requiring evaporation, while evaporation handles the concentrate that membranes cannot process efficiently.


Systems designed with this balance tend to achieve:

  • Lower overall operating costs
  • Higher water recovery
  • More stable long-term performance


FAQ

Q: Is RO enough for high-salinity wastewater treatment?

A: RO is effective up to a certain salinity level, but for very high TDS wastewater, evaporation is usually required to achieve stable performance.


Q: Which is more cost-effective, RO or evaporation?

A: RO is generally more energy-efficient, but evaporation becomes more cost-effective when treating high-salinity or concentrate streams that RO cannot handle.

Typical Process Flow of Industrial Wastewater Treatment Plants

Industrial wastewater treatment plants are designed to handle complex and variable wastewater streams generated from manufacturing processes. While each project has its own characteristics, most systems follow a similar industrial wastewater treatment process flow, combining physical, chemical, and advanced treatment technologies.


Understanding this typical process flow helps engineers and plant operators design systems that are both efficient and reliable in long-term operation.


Step 1: Equalization and Flow Balancing

The first stage in most industrial wastewater treatment systems is equalization. Wastewater from different production lines is collected and stored in an equalization tank to balance flow rate and pollutant concentration.


In practice, this step is often underestimated. In one surface treatment wastewater project, fluctuations in influent quality caused unstable downstream performance during early operation. After optimizing equalization capacity and mixing, the overall system became significantly more stable.


A properly designed equalization stage ensures consistent feed conditions for the following treatment processes.


Step 2: Chemical Pretreatment

Chemical pretreatment is typically used to remove suspended solids, heavy metals, and emulsified contaminants. Common processes include:

  • pH adjustment
  • Coagulation and flocculation
  • Chemical precipitation


For industries such as electroplating or metal finishing, this stage is critical for removing copper, nickel, chromium, and other heavy metals.


From an engineering perspective, pretreatment is not just about meeting discharge standards—it is about protecting downstream systems, especially membrane filtration units.


Step 3: Solid–Liquid Separation

After pretreatment, the system moves into solid–liquid separation. Technologies such as sedimentation tanks, lamella clarifiers, or DAF systems are commonly used to remove flocs formed during coagulation.


The choice of technology depends on wastewater characteristics:

  • High-density solids → sedimentation or lamella clarifier
  • Oil and light particles → dissolved air flotation (DAF)


In projects with complex wastewater composition, combining multiple separation methods can improve overall efficiency.


Step 4: Filtration and Polishing

Following clarification, filtration processes are used to further remove residual suspended solids and improve water quality.


This stage may include:

  • Sand filtration
  • Activated carbon filtration
  • Multimedia filters


Stable filtration performance is essential before entering advanced treatment stages, particularly when membranes are involved.


Step 5: Membrane Treatment for Water Reuse

In modern industrial water reuse systems, membrane technologies such as ultrafiltration (UF) and reverse osmosis (RO) are widely applied.


These systems remove dissolved salts, fine particles, and trace contaminants, producing high-quality water suitable for reuse in production processes.


In one industrial park wastewater project, integrating RO systems after pretreatment allowed the facility to achieve a high water recovery rate. However, early membrane fouling issues highlighted the importance of stable upstream treatment. Once pretreatment conditions were optimized, the system achieved consistent performance.


⇒Learn more about:

Industrial Reverse Osmosis Systems


Step 6: Concentrate Management and Advanced Treatment

Membrane processes generate concentrated brine that must be managed properly. Depending on discharge requirements and project goals, different solutions can be applied:

  • Discharge after further treatment
  • Evaporation and crystallization
  • Zero liquid discharge (ZLD) systems


For high-salinity wastewater, MVR evaporation technology is often used to reduce liquid waste and recover additional water.


⇒Related technology:

MVR Evaporation Systems


Engineering Perspective

While the typical wastewater treatment plant process flow appears straightforward, real-world performance depends heavily on how well each stage is integrated.


In practice, most operational issues are not caused by a single technology failure but by imbalances between process stages—for example, inadequate pretreatment leading to membrane fouling, or insufficient equalization causing unstable system loading.


A well-designed system is not just a sequence of technologies—it is a coordinated process built around actual wastewater characteristics and long-term operational requirements.


FAQ

Q: What is the typical process flow of industrial wastewater treatment?

A: Most systems include equalization, pretreatment, solid–liquid separation, filtration, membrane treatment, and concentrate management.


Q: Why is pretreatment important in wastewater treatment plants?

A: Pretreatment removes solids and contaminants that could damage downstream equipment, especially membrane systems, ensuring stable operation.

Wastewater Treatment Challenges in Semiconductor Manufacturing

Semiconductor manufacturing relies heavily on water—especially ultrapure water (UPW)—for wafer cleaning, etching, and rinsing. As production scales up, so does the complexity of wastewater generated. Addressing semiconductor wastewater treatment challenges has become a critical priority for facilities aiming to maintain compliance, reduce costs, and enable water reuse.


Complex and Variable Wastewater Composition

One of the main challenges in wastewater treatment for semiconductor manufacturing is the highly variable composition of wastewater streams.


Different production steps generate wastewater containing:

  • Acids and alkalis
  • Fluoride compounds
  • Photoresist residues
  • Trace heavy metals such as copper and nickel
  • High total dissolved solids (TDS)


Because these streams differ significantly, a single treatment approach is rarely sufficient. In practice, effective systems rely on segregation of wastewater streams to allow targeted treatment.


Sensitivity of Advanced Treatment Systems

Semiconductor wastewater treatment often requires advanced technologies such as membrane filtration and reverse osmosis (RO) to achieve reuse-grade water quality.


However, these systems are highly sensitive to feedwater conditions.


In one industrial wastewater reuse project with characteristics similar to semiconductor applications, early operation showed rapid membrane fouling and unstable pressure. Investigation revealed that inconsistent pretreatment allowed fine particles and residual organics to enter the membrane system.


After optimizing coagulation, filtration, and process control, the system stabilized and achieved the expected industrial water reuse performance.


This reflects a key engineering insight:

membrane systems perform reliably only when upstream treatment is stable and well-controlled.


⇒Learn more about:

Industrial Reverse Osmosis Systems


High Salinity and Concentrate Management

Another major challenge is managing high-salinity wastewater streams generated after membrane treatment.


As facilities push for higher water recovery rates, the remaining concentrate becomes more difficult to handle. High TDS levels can lead to scaling, reduced membrane efficiency, and limited discharge options.


In many cases, additional treatment steps such as evaporation are required to manage concentrate effectively.


⇒Related technology:

MVR Evaporation Systems


Integrating membrane systems with evaporation technologies allows facilities to increase recovery rates while maintaining stable operation.


Balancing Water Reuse and System Stability

While many semiconductor plants aim for aggressive water reuse targets, pushing systems beyond their stable operating range can create new challenges.


High recovery designs without sufficient control may result in:

  • Increased fouling and scaling
  • Higher chemical consumption
  • Frequent system downtime


From an engineering perspective, the goal is not maximum recovery, but optimal recovery—where water reuse is balanced with long-term system reliability.


Operational Complexity and Process Control

Semiconductor wastewater treatment systems are often complex, involving multiple treatment stages and strict process control requirements.


Small variations in pH, chemical dosing, or flow distribution can significantly impact overall performance. This makes automation, monitoring, and operator training essential for maintaining consistent treatment results.


In real-world projects, systems with strong process control strategies tend to perform more reliably and maintain compliance over time.


Engineering Perspective

Addressing industrial wastewater treatment challenges in semiconductor manufacturing requires a holistic approach.


Successful systems typically include:

  • Segregation of different wastewater streams
  • Robust pretreatment to protect advanced processes
  • Integration of membrane and thermal technologies
  • Flexible design to handle variability
  • Focus on long-term operational stability


Facilities that consider these factors early in project planning are better positioned to achieve both compliance and sustainable water reuse.

Wastewater Treatment Solutions for Electroplating Industry

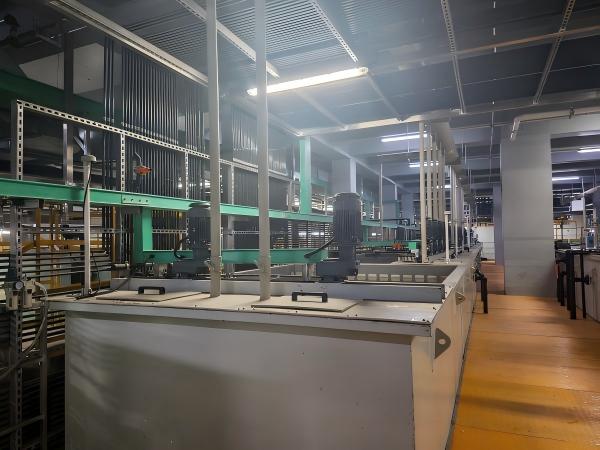
Electroplating is a critical process in modern manufacturing, but it also generates some of the most challenging industrial wastewater streams. Effective electroplating wastewater treatment solutions are essential not only for environmental compliance but also for improving water reuse and operational efficiency.


In this article, we explore how industrial facilities can address the complexity of electroplating wastewater through practical engineering approaches and proven treatment technologies.


Why Electroplating Wastewater Is Difficult to Treat

Electroplating wastewater typically contains a mixture of heavy metals, oils, surfactants, and suspended solids. Common contaminants include:

  • Copper, nickel, chromium, and zinc
  • Cyanide (in some processes)
  • Organic additives and surfactants
  • High total dissolved solids (TDS)


These pollutants vary depending on plating processes such as nickel plating, chromium plating, and precious metal finishing. This variability makes industrial wastewater treatment for electroplating plants particularly challenging.


In many cases, a single treatment method is not sufficient. Instead, a combination of physical, chemical, and advanced treatment technologies is required.


Typical Treatment Process for Electroplating Wastewater

A reliable electroplating wastewater treatment system usually includes multiple stages:


1. Chemical Pretreatment

pH adjustment, coagulation, and chemical precipitation are used to remove dissolved heavy metals by converting them into insoluble hydroxides.


2. Solid–Liquid Separation

Clarification processes such as lamella clarifiers or DAF systems remove the formed sludge and suspended solids.


3. Filtration and Polishing

Multimedia filters or activated carbon systems improve water quality before advanced treatment.


4. Membrane Treatment for Reuse

Advanced systems such as reverse osmosis (RO) are used to remove dissolved salts and produce reusable water.


⇒Learn more about:

Industrial Reverse Osmosis Systems


Achieving Water Reuse in Electroplating Plants

With increasing pressure on water resources, many facilities are moving toward industrial water reuse systems for electroplating wastewater.


In a surface treatment industrial park project, wastewater from multiple plating processes contained nickel, copper, chromium, as well as oils and suspended solids from pretreatment stages. The treatment system was designed to meet strict discharge standards while achieving a high water reuse rate.


During initial operation, fluctuations in influent quality caused instability in downstream processes. After optimizing pretreatment and solids removal, the system achieved stable operation, allowing treated water to be reused within the plant.


This project highlights an important insight:

stable pretreatment is the foundation of successful water reuse in electroplating wastewater treatment.


Managing High-Salinity Wastewater and Concentrate

Even after membrane treatment, electroplating wastewater systems often generate high-salinity concentrate streams.


When discharge is restricted or reuse targets are high, facilities may adopt zero liquid discharge (ZLD) solutions for electroplating wastewater. In such systems, evaporation technologies are used to further treat concentrated brine.


⇒Related technology:

MVR Evaporation Systems


By integrating membrane systems with evaporation, plants can significantly reduce liquid discharge and improve overall water recovery.


Engineering Perspective

From an engineering standpoint, the effectiveness of an electroplating wastewater treatment solution depends on how well the system handles variability.


In real-world projects, key success factors include:

  • Proper segregation of wastewater streams
  • Robust pretreatment for heavy metal removal
  • Stable solid–liquid separation
  • Integration of membrane and advanced treatment technologies


Systems that are designed only for average conditions often struggle under fluctuating loads, leading to higher operating costs and unstable performance.


FAQ

Q: What is the best treatment method for electroplating wastewater?

A: There is no single best method. Most systems combine chemical pretreatment, clarification, filtration, and membrane technologies to achieve stable performance.


Q: Can electroplating wastewater be reused?

A: Yes. With advanced treatment such as reverse osmosis, electroplating wastewater can be treated and reused for industrial processes.

Water Treatment Solutions for Chemical Manufacturing Plants

Chemical manufacturing plants generate some of the most complex wastewater in industrial production. With diverse raw materials, multiple process steps, and variable operating conditions, designing effective water treatment solutions for chemical manufacturing plants requires a practical, experience-based approach.


Beyond meeting discharge standards, many facilities are now focused on industrial water reuse systems, cost control, and long-term operational stability.


Why Chemical Wastewater Is Challenging

Unlike relatively consistent industrial streams, chemical plant wastewater treatment must deal with:

  • High COD and complex organic compounds
  • Variable pH conditions
  • Dissolved salts and high total dissolved solids (TDS)
  • Heavy metals and process-specific contaminants


In many projects, wastewater characteristics fluctuate significantly depending on production schedules. This variability is one of the main reasons why standard treatment designs often fail to perform consistently.


A Practical Treatment Approach

A reliable industrial wastewater treatment system for chemical plants typically includes multiple stages:


1. Equalization and Segregation

Balancing flow and separating high-strength streams helps stabilize downstream processes.


2. Chemical and Biological Pretreatment

Coagulation, flocculation, and in some cases biological treatment are used to remove organics and reduce pollutant load.


3. Solid–Liquid Separation

Clarification ensures that suspended solids are removed before advanced treatment.


4. Advanced Treatment for Reuse

Membrane technologies such as reverse osmosis (RO) are widely used to remove dissolved salts and produce reusable water.


Moving Toward Water Reuse

In recent projects, many chemical manufacturers have shifted from simple compliance to water reuse and recovery strategies.


In one industrial wastewater treatment project with characteristics similar to chemical manufacturing, wastewater contained mixed contaminants including dissolved salts, residual organics, and suspended solids. During early operation, unstable pretreatment led to frequent membrane fouling and reduced system efficiency.


After optimizing pretreatment and improving solids removal, the membrane system achieved stable performance and enabled consistent water reuse within the plant.


This experience highlights a key point:

water reuse in chemical wastewater treatment depends more on stability than on technology selection alone.


Handling High-Salinity Wastewater

As reuse rates increase, managing high-salinity wastewater becomes a critical challenge.


Reverse osmosis systems can recover a large portion of water, but they produce concentrated brine streams that require further treatment. In chemical plants with strict discharge limits, this concentrate cannot be discharged directly.


In such cases, integrating evaporation systems is often necessary.


By combining membrane systems with evaporation, facilities can significantly reduce wastewater volume and move toward zero liquid discharge (ZLD).


Balancing Cost and Performance

One of the most common questions in industrial water treatment for chemical plants is how to balance cost and performance.


In practice, overly complex systems may increase capital and operating costs without delivering proportional benefits. On the other hand, under-designed systems often lead to instability and higher long-term expenses.


From an engineering perspective, the most effective solutions are those that:

  • Match technology to actual wastewater characteristics
  • Optimize pretreatment to protect advanced systems
  • Balance water recovery with operational stability
  • Minimize energy consumption in high-load processes


In real-world applications, successful chemical wastewater treatment solutions are rarely defined by a single technology.


Instead, they are built on:

  • Careful analysis of wastewater composition
  • Flexible system design
  • Integration of multiple treatment stages
  • Focus on long-term operation rather than short-term targets


Facilities that approach water treatment as an operational system—rather than a standalone project—are more likely to achieve sustainable performance.


FAQ

Q: What is the best water treatment solution for chemical manufacturing plants?

A: There is no single solution. Most systems combine pretreatment, clarification, membrane filtration, and sometimes evaporation depending on wastewater characteristics.


Q: Can chemical plant wastewater be reused?

A: Yes. With proper treatment design, including RO and advanced processes, wastewater can be reused for various industrial applications.